INNOVATIONS IN COMPACT FIBER UNIT DESIGN

Intermittent Bonded Ribbon Production Line Available For Sale

A specified speed of 600 m/min gives this equipment considerable production capacity for optical-fiber applications. Before making purchasing plans, buyers should verify the actual speed, configuration, and operating conditions with the manufacturer.

Shanghai Weiye OFC supplies equipment designed specifically for producing rollable ribbons containing 12 or 16 fibers. The published product information covers capabilities, technical details, and supplied systems, helping U.S. buyers begin evaluating the equipment against their manufacturing needs.

Review the listed configuration in the product description, then contact the supplier about pricing, installation, and options specific to your project. Doing so can clarify which specifications and options are relevant to your facility and production objectives.

Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. provides its business address as 201 Minyi Road, Songjiang District, Shanghai. Use the product page for initial reference and verify current technical and commercial information directly with the company. A detailed quotation request can help advance your equipment evaluation.


Important Points To Consider

  • The stated operating speed is 600 m/min, although the manufacturer should confirm the applicable conditions.
  • This equipment supports production of 12-fiber and 16-fiber rollable ribbon formats.
  • Information about equipment functions, specifications, and included systems appears on the product page.
  • Request details about pricing, installation requirements, and project-specific customization.
  • A company address in Shanghai’s Songjiang District is included in the supplier information.

Overview Of The Intermittent Bonded Ribbon Production Line

According to the supplier, the equipment is designed for rollable IBR configurations containing 12 or 16 fibers. Its product page specifies a construction speed of 600 m/min and a fiber diameter of Ф245 μm ±10 μm. Because these figures represent stated machine specifications, buyers should verify achievable speeds and operating conditions with the manufacturer.
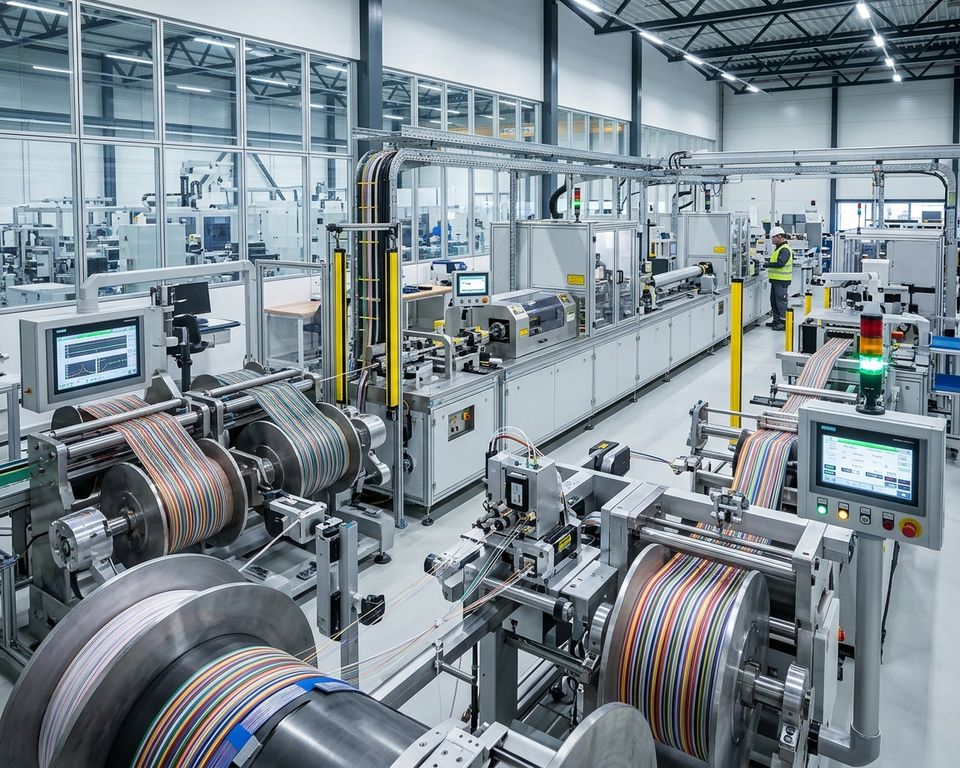
Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Designed To Produce Twelve- And Sixteen-Fiber Rollable Ribbons

Two fiber-count options are supported by the configuration for manufacturing rollable ribbons. Buyers can use these options as a starting point for checking compatibility with target formats, fiber sizes, and handling requirements.

How Intermittent Adhesive Bonding Allows Flexible Fiber Configurations

According to examples in the patent, fibers are arranged in adjacent subunits with adhesive connections applied periodically. The patent provides an example of adhesive-bond intervals ranging between 10 mm and 1,000 mm. This differs from a continuously bonded structure in which the connection extends across the full ribbon length.

These intermittent adhesive connections allow the assembly to change from a relatively flat configuration into rolled, curled, or folded forms. The specified spacing illustrates the patented design concept rather than confirmed production-machine settings.

  • Machine details: A choice of 12 or 16 fibers, a listed operating speed of 600 m/min, and a specified diameter of Ф245 μm ±10 μm.
  • Patent example: Illustrative spacing between adhesive bonds of 10 mm to 1,000 mm.
  • Design benefit: Flexible handling across several possible shapes.

Applications In Optical Fiber Cable Manufacturing

Adjustable fiber layouts may allow cable designers to combine convenient splice access with space-efficient packaging. The patent outlines a configuration that maintains fiber organization while allowing portions to move between adhesive connection points during cable assembly.

High Fiber Density And Compact Cable Designs

An optical fiber ribbon may remain flat during mass fusion splicing and subsequently fold or roll for installation in a smaller cable. The patent identifies opportunities for reduced cable dimensions and a greater proportion of fiber area relative to the cable’s cross-sectional area. The results achieved in practice depend on the complete cable construction and its intended use.

Organizing Fiber Ribbons To Support Efficient Fusion Splicing

This design supports orderly fiber handling during splicing while providing flexibility for subunit movement in the assembly process. The manufacturer’s material-handling specifications identify payoff reel capacities of 25.2 km and 50.4 km of fiber. Buyers can evaluate these capacities against their production requirements and existing handling arrangements.

Design detail Possible application Consideration for buyers
Flat fiber configuration Mass fusion splicing Verify the needs of your splicing process
Ribbon configuration that folds or rolls Space-efficient cable packaging Examine the complete cable design
Payoff reels with capacities of 25.2 km and 50.4 km Material-handling preparation Align reel capacities with operating needs

Production Line Specifications And Performance

Compare the equipment’s published performance figures with your manufacturing requirements before requesting a quotation. Installation preparations should also account for suitable reels and the utilities available at the production site.

Speed, Diameter, And Attenuation

The stated construction speed is 600 m/min. The specified fiber diameter is Ф245 μm ±10 μm, while additional attenuation is stated as ≤0.01 dB/km at 1550 nm. Confirm the measurement conditions and expected performance directly with the manufacturer.

Compatibility With Payoff And Take-Up Reels

Two payoff reel sizes are offered, with each full reel limited to 10 kg. The take-up assembly supports a T-type reel as well as a fiber-optic reel. Verify that your selected reel configuration is compatible with the facility’s material-handling process.

Site Utilities And Environment

The machine requires a three-phase, five-wire electrical supply rated at 380 V ±10%. Its specified operating environment is enclosed, clean, dry, and protected from drafts, with temperatures of 15 to 25°C and relative humidity no higher than 85%. Nitrogen must be supplied at 7 bar with 99.99% purity, together with compressed air at 6 bar. Check all utility connections in advance of installing the equipment.

Specification Published requirement Installation planning note
Reels for fiber payoff Ф236 × Ф25.4 × 108 mm; Ф267 × Ф25.4 × 180 mm; maximum full-reel weight ≤10 kg Verify reel dimensions and weight
Reel used for take-up T-type dimensions of Φ410 × Φ50.8 × 391 mm, or a fiber-optic reel Confirm compatibility with your selected format
Electrical and environmental requirements 380 V ±10%; 15 to 25°C; relative humidity ≤85% Provide a clean, dry area without drafts
Gas utility supply Nitrogen at 7 bar and 99.99% purity; compressed air at 6 bar Verify gas supply capacity before installation

Equipment For Fiber Payoff And Gathering

Optical fibers are guided toward the forming section by the payoff and gathering components. The associated controls help maintain a steady supply of fiber while reducing handling risks.

Sixteen-Spool Payoff With Tension Control

The payoff assembly holds 16 spools and provides traversing along with separately adjustable tension settings. The permitted weight for an individual spool is up to 10 kg. The technical details list 0.4 to 2 N tension with ±0.02 N accuracy, together with a 550 W motor. Because a separate overview states 40 to 150 g with ±2 g accuracy, ask the manufacturer to clarify the correct values for your intended setup.

Fiber Guiding, Break Detection, And Electrostatic Control

The forming area receives fibers through U-groove guides, multi-groove gathering rollers, and devices designed to prevent jumping. A break-detection system and alarms notify operators when problems occur. Safe handling is supported by protective guards and a pneumatic clamping mechanism. At the fiber exit, a rod-style electrostatic dust collector is installed, while anti-static equipment helps manage dust along the gathering route.

Component Listed detail Intended function
Payoff Capacity for 16 spools, each weighing up to 10 kg Feeds optical fibers with traversing movement
Tension and motor 0.4 to 2 N with ±0.02 N accuracy; 550 W Supports regulated payoff of fibers
Fiber guidance and safety features Grooved rollers, alarms, guards, and pneumatic clamping Guides fiber movement and assists material handling
Electrostatic management Rod-type dust collector and anti-static equipment Helps reduce dust near fiber routes

Precision Molding And Intermittent Adhesive Dispensing

Operators can adjust adhesive positioning and mold alignment through the forming platform. Available adjustments help configure the process for each required ribbon format.

Ribbon Formation Using An Adjustable IBR Mold Platform

Three mold sets are provided for ribbon formation, and each accommodates as many as five Nordson EFD jet valves. The mold adjustment range extends from 0 to 15 mm, while the mold base can be maintained between 20°C and 60°C. Precision valve groups mounted on sliding tables allow fine positioning and accurate application of adhesive dots.

Adjustable Nozzle Configurations For Twelve- And Sixteen-Fiber Ribbon Production

The 12-fiber configuration employs a 5+5+1 valve arrangement. The 16-fiber format is produced using a 5+5+5 valve layout. Operators can adjust adhesive-dot spacing and the number of dots through the interface to match the selected optical fiber ribbon design. The process calls for a specialized adhesive suitable for both coating and curing.

Setting Format With 12 Fibers 16-Fiber Format
Valve arrangement 5+5+1 valve configuration Valve arrangement of 5+5+5
Mold positioning range 0 to 15 mm adjustment Adjustment range of 0 to 15 mm
Temperature of the mold base 20°C to 60°C operating range 20°C to 60°C operating range

Curing Bonded Fiber Ribbons With UV-LED Technology

Adhesive across the fiber assembly is cured through a sequence of UV exposure stages. The arrangement of the ovens and their published operating values provide buyers with information for evaluating process compatibility.

Pre-Curing And Main Curing Stages

Three dedicated LED-UV ovens rated at 800 W each perform the pre-curing operation. Each oven processes fibers supplied by a separate mold group before the material reaches the main 6 kW post-curing oven. The system uses adjustable shutters to help contain UV exposure and minimize nitrogen losses. Published specifications identify a dominant wavelength of 395 nm ±3 nm, a curing degree of at least 85%, and post-curing power of at least 2.5 kW.

Nitrogen Management And Curing Performance

The nitrogen flow rate and pressure can be adjusted by hand. Automatic functions also start nitrogen delivery during startup and stop it at shutdown. At production speed under continuous stable conditions, the specified lamp-array power consumption is no more than 80% of total power. These specifications provide a reference for comparing equipment, although testing conditions should be verified with the supplier. Ask whether different adhesives or materials require adjustments to the settings.

Visual Monitoring, Capstan, And Take-Up

Visual inspection and consistent winding help preserve fiber quality as material passes through the production line. The published operating settings also offer buyers useful criteria for comparing equipment against their cable production requirements.

Real-Time Inspection Of Fiber Colors And Adhesive Dot Placement

A microscope and camera provide enlarged images in real time. The display allows operators to check the sequence of fiber colors and confirm adhesive resin dots at each dispensing position. By examining the optical fiber ribbon during production, operators can detect potential issues ahead of winding.

Servo-Driven Traction And Precision Take-Up

A 1 kW AC servo motor powers the capstan’s Φ190 mm traction wheel. Metering accuracy is specified as better than 1‰. The adjustable tension range is 50 to 500 g, with control accuracy of ±5 g. These operating parameters help maintain careful fiber-ribbon handling as the material advances through the line.

The specified take-up speed is 600 m/min, and the maximum spool weight is 30 kg. Servo-controlled winding and traversing systems help maintain consistent material placement. The cable pitch setting allows continuous adjustment from 1 to 6 mm. Position detection and direction changes are supported by a photoelectric sensor. Confirm that the operating conditions and settings are suitable for your target cable design with the supplier.

Production Monitoring And Electrical Control Systems

Clear control functions help production staff manage settings, monitor system conditions, and prepare smooth stopping procedures. According to the manufacturer, the machinery incorporates Siemens controls alongside Schneider Electric switchgear.

PLC And Touchscreen Operation

Siemens S7-1200 and S7-1500 PLCs manage the ribbon manufacturing system through a 10.4-inch Siemens touchscreen. Low-voltage switchgear is supplied by Schneider Electric. The system supports both interlocked operation across the full production line and separate operation of individual units.

Process Settings, Warning Alarms, And Preset-Length Shutdowns

Through the touchscreen, operators can manage process settings, activate curing ovens, configure wire feeding, and view alarms. Additional displays provide lamp runtime, real-time current readings, curing-oven temperature, and total machine operating hours. The meter-counter calibration feature allows displayed counts to be aligned with the distance actually traveled.

A preset length can be entered to initiate slowing or stopping of the machine. This provides a practical way to control the end of a cable production run. Verify the available controls and configuration requirements with the supplier before purchasing.

Control-system feature Published specification Use
PLC and display Siemens S7-1200 and S7-1500 PLCs with a 10.4-inch touchscreen Configure settings and examine production data
Electrical components Schneider Electric low-voltage switchgear Provides support for system control
Monitoring and stopping Operating data for lamps, ovens, runtime, and meters; preset-length function Track operating conditions and initiate machine stopping or slowing

Materials, Process Compatibility, And Ribbon Quality

The selected adhesive influences coating uniformity and the quality of the finished ribbon. The manufacturer calls for a specialized adhesive intended for the machine’s coating and curing process instead of an ordinary multipurpose product.

Dedicated Adhesive For Bonding And Curing

The pressure-fed adhesive system provides independent valve switches so each supply path can be opened or closed as required. Precision pressure-regulating valves help maintain controlled adhesive delivery at each dispensing location. The specified air pressure is adjustable, with a required minimum of 0.5 MPa.

The adhesive lines are black to reduce the risk of UV-triggered reactions while the system operates and cures material. This protection is important because premature exposure may change adhesive properties before application to the fiber.

Before selecting materials for a secondary coating line, verify adhesive compatibility, production settings, and required surface-quality standards with the supplier. Ask how the recommended adhesive performs under your intended application conditions and expected production length. Clear process instructions can help maintain quality from initial setup through final production.

Installation Requirements And Included Documentation

Ensure the workspace and utility supplies are ready before scheduling the machine’s installation. The supplier’s specifications provide guidance for planning the production site and supporting consistent operation of the fiber-optic machinery.

Required Facility Conditions And Connections Provided By The Buyer

Install the machinery in a clean, dry, enclosed environment protected from drafts. Maintain a room temperature of 15 to 25°C and relative humidity no higher than 85%. The installation also requires nitrogen supplied at 7 bar with 99.99% purity and an air supply rated at 6 bar.

The equipment package does not include connecting cables or cable trays. The buyer must arrange the principal power feed-in cable. Before installation, check cable routing and utility capacity, particularly when the machine will be located near secondary coating operations.

Documentation For Operation, Installation, And Maintenance

The supplier includes documentation supporting machine installation, operation, and servicing. Review these records before startup to help staff plan work activities and identify necessary supplies.

  • Operating and instruction manuals together with the overall equipment layout drawing
  • Wiring and electrical schematic diagrams, plus installation and maintenance drawings
  • Purchased-component instructions and a wear-parts list to support service preparation

The supplied records support preparation for commissioning and routine servicing of the cable production machinery.

Selecting A Ribbon Production Line That Matches Your Manufacturing Requirements

First determine which finished ribbon products your business plans to offer. The machinery supports 12F and 16F formats and has a stated construction speed of 600 m/min. Compare those specifications with your expected product mix, production targets, and anticipated cable demand.

Before purchasing the machine, confirm that its take-up arrangement matches your requirements. A standard IBR reel measures Φ410 × Φ50.8 × 390 × Φ310 mm, accommodates a maximum weight of 30 kg, and allows cable pitch settings between 1 and 6 mm. Confirm that the listed reel dimensions, capacity, and pitch range are appropriate for your site and handling process.

Payoff reel compatibility also deserves attention. The listed choices include internationally standardized spools with capacities of 25.2 km, 50.4 km, and 63 km. Request precise reel measurements before selecting materials or determining production run lengths.

In addition to speed, consider power and gas utilities, suitable adhesives, and the available monitoring functions. For cable manufacturing, determine whether the configuration suits fiber cable, loose tube, or another planned application. Discuss machine configuration and commissioning arrangements with Shanghai Weiye before committing to the purchase. A thorough compatibility assessment can help prevent expensive modifications later.

Planning point Manufacturer-listed specification Buyer check
Formats and speed 12F and 16F formats; 600 m/min Compare with target production and product mix
Take-up configuration Maximum 30 kg; cable pitch of 1 to 6 mm Check reel compatibility and facility requirements
Payoff spools Capacities of 25.2 km, 50.4 km, and 63 km Confirm the precise reel measurements

How To Request A Quotation For The Intermittent Bonded Ribbon Production Line

U.S. buyers can evaluate a system offering 12F and 16F formats, a specified construction rate of 600 m/min, and specialized optical fiber ribbon-forming equipment. Use these specifications to determine whether the machine is appropriate for your intended cable application.

When requesting a quotation, provide the required ribbon format, expected output volume, preferred reels, and available site utilities. Also describe the fiber type and handling requirements so Shanghai Weiye can evaluate the proposed configuration.

Confirm the suitability of the adhesive, the LED wavelength specification of 395 nm ±3 nm, and expected curing results before purchasing. Discuss how the stated specifications affect your intended material and finished surface-quality objectives.

Consult the product page for the published equipment description. Verify the final configuration, shipment details, and installation commissioning with Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. The supplier provides its address as 201 Minyi Road, Songjiang District, Shanghai. Telephone 021-60701630 to discuss your manufacturing requirements. A detailed quotation inquiry helps define the next steps in purchasing.
JACKET ADHESION TESTING ON THE FIBER CABLE SHEATHING LINE

An intermittently bonded ribbon production system is used to manufacture flexible fiber groups for contemporary, high-count cable architectures. It ensures fibers are aligned for expedited mass fusion splicing, yet allows the fiber group to remain flexible within a compact cable core.

Unlike fully bonded ribbons, intermittent bonded ribbons feature localized bonds at predetermined intervals. This strategic placement allows fibers to remain aligned while the ribbon can bend and roll into circular loose tubes and other confined spaces.

Network engineers employ this method when faced with constraints in duct space, splice closures, and equipment racks. A meticulously crafted ribbon cable facilitates dense network deployments in data centers, telecom backbones, metro networks, FTTx feeder systems, and 5G transport networks.


Main Takeaways

  • A bonded ribbon production system supports compact and flexible fiber layouts.
  • Localized bonds keep optical fibers aligned while preserving ribbon flexibility.
  • Flexible ribbons help cable makers fit more fibers into compact circular cable designs.
  • Stable fiber order helps accelerate mass fusion splicing.
  • Ribbon cable technology serves data centers, telecom routes, and fiber access networks.

Intermittent Bonded Ribbon Production Line Overview

Intermittently bonded ribbon manufacturing allows the creation of fiber designs that combine high density with practical handling. This method involves applying bond points at controlled intervals, allowing for the movement of fiber subunits between these points.

The method enables the incorporation of a higher number of fibers within constrained duct spaces. It also helps maintain the organized ribbon structure, essential for efficient splicing and cable assembly processes.

How Does An Intermittently Bonded Optical Fiber Ribbon Work?

An intermittent bonded fiber ribbon connects adjacent fibers at specific intervals along its length. The segments between these bonds are left flexible, enabling the ribbon to adopt various configurations without rigidification.

The design is frequently known as a rollable, flexible, or spider web ribbon. It diverges from the conventional flat ribbon cable, which maintains a fixed profile along its entire length.

During splicing, the fibers can be arranged into a flat ribbon for mass fusion operations. In cable production, the same fibers form compact bundles, optimizing space utilization within the cable.

Why High-Density Fiber Networks Need Flexible Ribbon Technology

Network architects face the challenge of increasing capacity within densely populated conduits, data centers, and access routes. The flexible nature of a flat cable structure enables ribbon groups to be packed into smaller cable cores, preserving fiber order.

A fiber density ratio provides a critical metric for network builders, comparing the space occupied by fibers to the total cable area. Intermittent bonding helps increase this density ratio, allowing ribbon groups to occupy available spaces within the cable.

For installers, high-density fiber cables reduce the number of cables required for a given route. This design also supports high fiber counts without necessitating a rigid ribbon stack.

Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Ribbon Design Feature Flexible Bonded Design Traditional Continuous Ribbon
Bond pattern Separated bonds at controlled intervals Bonding maintained continuously along the ribbon
Fiber configuration between bond points Can bend, roll, or fold for dense packing Maintains a largely fixed flat profile
Splicing configuration Can return to a flat format for mass fusion splicing Already held in a fixed flat ribbon form
Cable packing role Allows compact and flexible subunit positioning Typically uses a fixed ribbon stack configuration
Common cable use Flexible flat cable and high-density fiber cable designs Standard flat ribbon cable designs

Construction And Material Requirements For Intermittent Bonded Ribbon

An intermittent bonded ribbon integrates precise fiber placement with adaptable bonding points. Its architecture facilitates dense cable configurations while allowing effortless separation during handling, routing, and splicing.

Choosing appropriate materials significantly influences ribbon width, peel characteristics, and durability. Each optical fiber subunit must maintain its fibers securely without imparting undue stiffness to the ribbon.

Optical Fiber Counts And Subunit Layout

Flexible bonded ribbons may support 4, 8, 12, 24, or up to 36 fibers. The choice of fiber count is determined by cable capacity, available duct space, and the requirements of subsequent mass fusion splicing.

A 12-fiber configuration often employs six subunits, with two adjacent fibers in each subunit. The fibers within a subunit may be in contact or separated by no more than one and a half times the fiber diameter.

Small gaps placed between subunits ensures ribbon flexibility. These gaps typically span from 5 to 100 micrometers, while the fibers remain aligned side by side across the ribbon width.

Construction Feature Typical Arrangement Manufacturing Purpose
Fiber count 4, 8, 12, 24, or as many as 36 fibers Supports required cable density and fusion splice capacity
Subunit configuration Two adjacent fibers per optical fiber subunit Allows controlled separation between fiber groups
Subunit fiber spacing Fibers touching or separated by up to 1.5 diameters Supports a small and consistent subunit profile
Gap between subunits 5 to 100 micrometers Allows greater movement and flexibility near bond points

UV-Curable Resin And Wet-On-Wet Bonding

The coating and bond systems frequently employ UV-curable resin systems. Wet-on-wet bonding involves applying the bond material to the uncured subunit coating, which then cures together under UV energy.

Wet-on-wet bonding produces a diffusion zone where the materials interact. For intermittent bonded ribbons, this zone can range from 2 to 50 micrometers, with 5 to 15 micrometers being the typical focused process range.

UV-curable resin materials can blend at the interface before curing. This encourages molecular entanglement between the bond and the optical fiber subunit coating, resulting in bonds that are both secure and flexible.

Main Equipment For Intermittent Bonded Ribbon Production

An optical ribbon line integrates advanced motion control with meticulous material handling. Each station ensures fibers remain aligned, clean, and stable from the initial payoff to the final winding.

The line equipment manages adjacent fiber placement, subunit coating, intermittent bonding, UV curing, cooling, inspection, and take-up. This sequential process enables manufacturers to produce flexible custom ribbon cable, preserving the integrity of the fiber order.

Fiber Payoff With Tension Control

Fiber payoff systems feed individual optical fibers at a consistent rate from spools. Guides, rollers, and tension sensors prevent sudden pulls, averting twist, slack, or uneven spacing.

During ribbon production, maintaining balanced fiber paths before alignment is critical. Stable tension is essential for forming flat subunits and ensuring accurate color sequence control.

Discrete Bond Applicator And Coating Die

A coating die places a UV-curable material around groups of two or more fibers. This material defines subunits while maintaining fibers in a flat, parallel layout.

The discrete bond applicator subsequently deposits a second resin between neighboring subunits at planned intervals. This spacing allows the ribbon to flex and separate when needed, a critical aspect of custom ribbon cable design.

Production Equipment Primary Function Process Benefit
Payoff tension system Delivers fibers while maintaining regulated tension Minimizes twisting and uneven fiber loading
Coating die Creates coated optical fiber subunits Supports stable subunit width and geometry
Intermittent bond applicator Deposits resin at set intervals Provides controlled flexible bonds between subunits
UV curing, cooling, and take-up unit Cures and cools the ribbon before inspection and winding Protects bond quality and preserves fiber order

UV Curing, Cooling, And Ribbon Take-Up Equipment

UV energy cures the subunit coating and intermittent bonds while the resin is wet. This wet-on-wet process forms a cohesive interface between materials, influencing bond strength.

Cooling equipment lowers ribbon temperature before inspection and winding. The fiber ribbon line may also employ vision checks to monitor width, bond position, and surface quality.

Take-up equipment winds the finished ribbon with low, even tension. Proper winding preserves the finished bonded structure, ensuring the custom ribbon cable is ready for later cabling, splicing, or connector assembly.

Fiber Preparation, Alignment, And Color Sequence Control

Reliable ribbon cable production starts with fiber preparation. Each strand must enter the assembly clean, centered, and in the correct sequence before the coating and bonding processes commence.

Managing Fiber Identification During Splicing And Maintenance

Consistent fiber color identification is indispensable for splicing, testing, and maintenance operations. The standard 12-fiber sequence, typically consisting of blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua, facilitates swift identification.

When fiber counts increase, the sequence may be repeated within controlled subunits. This method ensures that each ribbon cable remains organized within splice trays, closures, and cable connector layouts.

Fiber Number Fiber Identification Color Process Purpose
1 Standard blue Marks the first position in the standard color order
2 Standard orange Provides rapid visual identification
3 Standard green Helps preserve the established fiber order
04 Brown Helps verify subunit placement
05 Standard slate Provides distinct mid-sequence marking
6 White Improves visibility during inspection
07 Standard red Improves traceability in splicing records
8 Black Helps technicians recognize sequence position in trays
09 Standard yellow Aids field restoration work
Position 10 Standard violet Helps distinguish later positions in the standard sequence
11 Standard rose Helps maintain clarity in higher-count ribbon layouts
12 Aqua Finishes the standard 12-fiber color sequence

Preventing Fiber Twisting And Uneven Tension

Payoff units and guides are instrumental in maintaining fibers in a flat, side-by-side configuration. This prevents twist, crossing, and gaps that could alter the ribbon’s width or distort the bond pattern.

Production personnel carefully check tension across every path before the fibers reach the coating die. Proper alignment is critical for mass fusion splicing and ensures the finished ribbon cable fits its intended cable connector system.

Intermittent Bond Application And UV Curing Process

Intermittent bonding connects fiber subunits without solidifying the ribbon into a rigid form. This method facilitates compact routing and ensures dependable handling within a flexible flat cable. It also aids in maintaining the planned fiber layout during subsequent cable assembly.

Applying Bonds At Predetermined Intervals

Bond applicators place resin at intervals ranging from 10 mm to 1,000 mm. The bond locations may stagger along the ribbon’s length. This arrangement provides support to adjacent subunits while allowing sufficient free length for movement.

The bond applicator delivers a measured amount of UV-curable resin at each bond point. Bonds often exhibit a diamond-like shape, with wider centers and narrower ends. The tapered ends reduce sudden stress transitions when the cable bends or twists.

Creating Flexible And Strong Bond Interfaces

Wet-on-wet bonding involves applying a second material before the first subunit coating cures. The uncured layers can blend before undergoing a shared UV curing step. This approach fosters a gradual interface, unlike a sharp material boundary.

The resulting material gradient affects various properties, including color, Young’s modulus, and surface friction. Bond ends may feature saddle-like surfaces with both convex and concave curves. These features improve resistance to bond peeling while facilitating separation when required.

Controlling Curing Performance

The UV lamps must supply consistent energy across the ribbon. Factors such as line speed, lamp output, resin volume, and exposure time impact the bond’s quality. Selecting the right UV-curable resin ensures rapid curing without compromising the fiber coating.

Process personnel carefully track bond shape, cure level, and ribbon flexibility during production. The cured cable should transition smoothly from a flat plane to various forms without bond damage. Controlled curing ensures consistent handling throughout winding and downstream processing.

Quality Control For Flexible Flat Cable And Fiber Ribbon Output

Maintaining the integrity of each flat ribbon cable is a meticulous process. It involves checking the cable’s flexibility and its readiness for subsequent splicing operations. During production, operators assess the fiber count, color sequence, and precise positioning of each fiber. They also evaluate the cable’s winding condition, ensuring its optimal state for assembly.

Routine inspection is essential in identifying any defects in the coating, uneven tension, or misplaced bonds. These issues, if left unaddressed, could compromise the cable’s performance in subsequent stages of production.

Inspection Of Bond Spacing, Ribbon Width, And Thickness

The spacing between bonds is a critical parameter, requiring adherence to a specific design range. This spacing is essential for the cable’s flexibility, ensuring that the fibers remain aligned within their designated subunits during bending.

Inspection protocols are in place to confirm that each bond correctly connects adjacent subunits. This attention to detail ensures that the ribbon lays flat, facilitating smooth mass fusion splicing processes.

Inspection Point Items Checked Production Value
Fiber sequence identification Fiber number, color order, and placement Helps ensure accurate splicing and maintenance
Bond pattern Bond position, interval, and connection between subunits Supports organized fibers without sacrificing flexibility
Ribbon profile Width, thickness, and flatness Supports compatibility with handling and splice equipment
Surface condition UV curing condition, coating coverage, and surface defects Reduces handling damage during winding

Optical And Mechanical Performance Testing

Mechanical testing focuses on bond separation, cohesive strength, elongation, and handling behavior. These evaluations are essential to confirm that the manufacturing process controls are consistent across similar designs of flat cables.

Optical testing encompasses evaluations after bonding and curing. It ensures that the core, cladding, primary coating, secondary coating, and color layer are adequately protected throughout the manufacturing process.

Attenuation measurements and splice-handling tests are integral to routine inspections. The quality of winding is also scrutinized to ensure that the finished flat ribbon cable is in a controlled condition for assembly.

Precision Winding, Automation, And Production Efficiency

High-efficiency ribbon production relies on a unified production line. Each stage, from fiber payoff to inspection and take-up, must harmonize seamlessly. This synchronization ensures the preservation of fiber geometry and facilitates consistent output, critical for high-speed data transmission cables.

Line Synchronization And Process Data Monitoring

Control systems integrate payoff speed, fiber tension, resin delivery, bond placement, UV curing, cooling, and take-up. Adjustments are made in real time to maintain ribbon stability when speed variations occur at any station.

Production records track fiber color sequences, bond intervals, cure settings, ribbon dimensions, and winding status. This detailed history allows operators to track the production of each custom ribbon cable.

  • Payoff tension prevents fiber stretch and slack.
  • Controlled bond timing maintains regular intervals between bond points.
  • Dimensional checks detect width or thickness deviations promptly.
  • Winding records support lot traceability and downstream handling.

Winding Ribbon For Downstream Cable Production

A precision cable winder helps ensure the ribbon is wound onto a spool with uniform tension and controlled movement. This method prevents edge crushing, layer crossing, and sudden pulls during subsequent cable processing.

Finished ribbon structures may be stacked, rolled, or loaded into central tube and loose tube designs. These configurations enable the creation of high-speed data transmission cables, even in areas where duct additions are impractical.

When producing custom ribbon cable, the winding pattern must align with subsequent processes. Proper spool buildup is essential for smooth payout during stranding, tube loading, and cable assembly.

Monitoring Area Primary Control Focus Resulting Benefit
Optical fiber payoff Stable tension and correct color sequence Consistent ribbon organization during cable assembly
Bond application Consistent spacing and resin volume Consistent flexible behavior in downstream operations
UV cure stage Regulated UV intensity and exposure duration Properly cured bonds before ribbon winding
Cable winding system Uniform traverse with controlled spool tension and layering Smooth payout for central tube or loose tube loading

Ribbon Cable Applications, Fusion Splicing, And Connector Planning

Ribbon fiber is widely used in dense links within data centers, telecom backbones, metro rings, and FTTx feeder routes. It also excels in indoor FTTH runs, 5G fronthaul, and outdoor point-to-point networks where space is at a premium.

A meticulously planned ribbon cable assembly enables crews to manage high fiber counts efficiently, without increasing bulk. Each high-speed data transmission cable must align with the site’s route, enclosure space, and future expansion plans.

Mass Fusion Splicing Advantages

A ribbon fusion splicer allows the joining of an entire ribbon in a single operation. For a 12-fiber ribbon, a matching cleaver can prepare all 12 fibers simultaneously before the automated fusion process commences.

Mass fusion processing lowers handling time and ensures consistent fiber alignment. Splice loss is reported to remain below 0.05 to 0.10 dB per fiber, contingent upon controlled preparation, cleaning, and machine settings.

Loose tube cable, on the other hand necessitates a different strategy at the splice cassette. Technicians must separate the fibers, then splice them individually, which prolongs the ribbon cable assembly process.

Dense Link Connection Planning

High-density fiber links often employ MPO or MTP trunks, harnesses, fanout cables, and cassette modules. The chosen cable connector must align with the fiber count, polarity method, connector gender, and fiber type.

System planning must also account for transceiver requirements and the full link loss budget. A high-speed data transmission cable, when used with parallel optics, demands a clear polarity path from equipment port to patch panel.

Planning Item Primary Control Common Application
Number of ribbon fibers Required splice capacity and cassette configuration Backbone links using 12-fiber or 24-fiber ribbons
MPO/MTP cable connector Connector polarity, gender, and port compatibility Data center trunk links and 5G equipment areas
Harness or fanout cable Transition from multi-fiber connections to single-fiber ports Network switch connections and patch fields
Link loss budget Permitted optical loss across splices, connectors, and fiber High-speed data transmission cable routes

Shanghai Weiye OFC Equipment For Fiber Ribbon Production Lines

Shanghai Weiye OFC Equipment, also known as SHWY, specializes in machinery for the production of optical fibers and cables, serving markets in the United States and globally. Its offerings are designed to maintain stable production, facilitate clear operator control, and enable seamless integration into production lines.

For initiatives requiring an intermittent bonded ribbon production line, SHWY equips each phase of ribbon handling, curing, and winding with suitable machinery.

SHWY Optical Fiber And Cable Machinery Experience

Established in 1998, SHWY’s journey in the industry has been marked by significant milestones. By 2012, its annual turnover surpassed 200 million CNY, strengthening its position within a prominent Chinese fiber and cable conglomerate as a joint venture.

In 2020, SHWY transitioned to independence, relocating to a state-of-the-art facility in central Shanghai. This move underscored its commitment to advancing equipment research, manufacturing, and process application while supporting operational stability.

SHWY Production Equipment Portfolio

SHWY offers a diverse range of equipment, including fiber draw towers, coloring machines, secondary coating lines, SZ stranding equipment, and cable sheathing lines. Notably, it also features a fiber ribbon line tailored for flat, high-count fiber formats.

Within ribbon cable production, a cable precision winder plays a critical role in maintaining orderly package buildup and controlled tension. This ensures safer transport and more consistent feeding into subsequent cable production stages.

Additional SHWY equipment includes FTTH lines, indoor cable equipment, and OPGW fiber-in-stainless-steel-tube systems. These options enable manufacturers to integrate an intermittent bonded ribbon production line with complementary cable processes.

Final Thoughts

A complete intermittent bonded ribbon line brings together fiber alignment, controlled bonding, UV curing, inspection, and precision winding into a unified process. Each step maintains organized fiber positioning while maintaining the necessary bendability for dense cable designs. This combination is critical for the creation of high-density optical networks.

The resultant ribbon cable supports efficient mass fusion splicing and organized fiber management. It is ideal for applications with high fiber counts, confined ducts, limited tray space, and frequent splice points. This makes it a cornerstone in many high-density ribbon cable routes.

Comprehensive project planning reaches beyond the production line. It encompasses the cable structure, closure capacity, fusion tools, test methodologies, labeling, and restoration records. These elements must align with the planned network architecture for seamless integration.

Related: How to Choose the Right Fiber Cable Sheathing Line for FTTH Projects
         Fiber Draw Tower Software and Control Interfaces