An intermittently bonded ribbon production system is used to manufacture flexible fiber groups for contemporary, high-count cable architectures. It ensures fibers are aligned for expedited mass fusion splicing, yet allows the fiber group to remain flexible within a compact cable core.
Unlike fully bonded ribbons, intermittent bonded ribbons feature localized bonds at predetermined intervals. This strategic placement allows fibers to remain aligned while the ribbon can bend and roll into circular loose tubes and other confined spaces.
Network engineers employ this method when faced with constraints in duct space, splice closures, and equipment racks. A meticulously crafted ribbon cable facilitates dense network deployments in data centers, telecom backbones, metro networks, FTTx feeder systems, and 5G transport networks.
Fiber Coloring Machine
FTTH Cable Production Line
Fiber Draw Tower
Main Takeaways
- A bonded ribbon production system supports compact and flexible fiber layouts.
- Localized bonds keep optical fibers aligned while preserving ribbon flexibility.
- Flexible ribbons help cable makers fit more fibers into compact circular cable designs.
- Stable fiber order helps accelerate mass fusion splicing.
- Ribbon cable technology serves data centers, telecom routes, and fiber access networks.
Intermittent Bonded Ribbon Production Line Overview
Intermittently bonded ribbon manufacturing allows the creation of fiber designs that combine high density with practical handling. This method involves applying bond points at controlled intervals, allowing for the movement of fiber subunits between these points.
The method enables the incorporation of a higher number of fibers within constrained duct spaces. It also helps maintain the organized ribbon structure, essential for efficient splicing and cable assembly processes.
How Does An Intermittently Bonded Optical Fiber Ribbon Work?
An intermittent bonded fiber ribbon connects adjacent fibers at specific intervals along its length. The segments between these bonds are left flexible, enabling the ribbon to adopt various configurations without rigidification.
The design is frequently known as a rollable, flexible, or spider web ribbon. It diverges from the conventional flat ribbon cable, which maintains a fixed profile along its entire length.
During splicing, the fibers can be arranged into a flat ribbon for mass fusion operations. In cable production, the same fibers form compact bundles, optimizing space utilization within the cable.
Why High-Density Fiber Networks Need Flexible Ribbon Technology
Network architects face the challenge of increasing capacity within densely populated conduits, data centers, and access routes. The flexible nature of a flat cable structure enables ribbon groups to be packed into smaller cable cores, preserving fiber order.
A fiber density ratio provides a critical metric for network builders, comparing the space occupied by fibers to the total cable area. Intermittent bonding helps increase this density ratio, allowing ribbon groups to occupy available spaces within the cable.
For installers, high-density fiber cables reduce the number of cables required for a given route. This design also supports high fiber counts without necessitating a rigid ribbon stack.
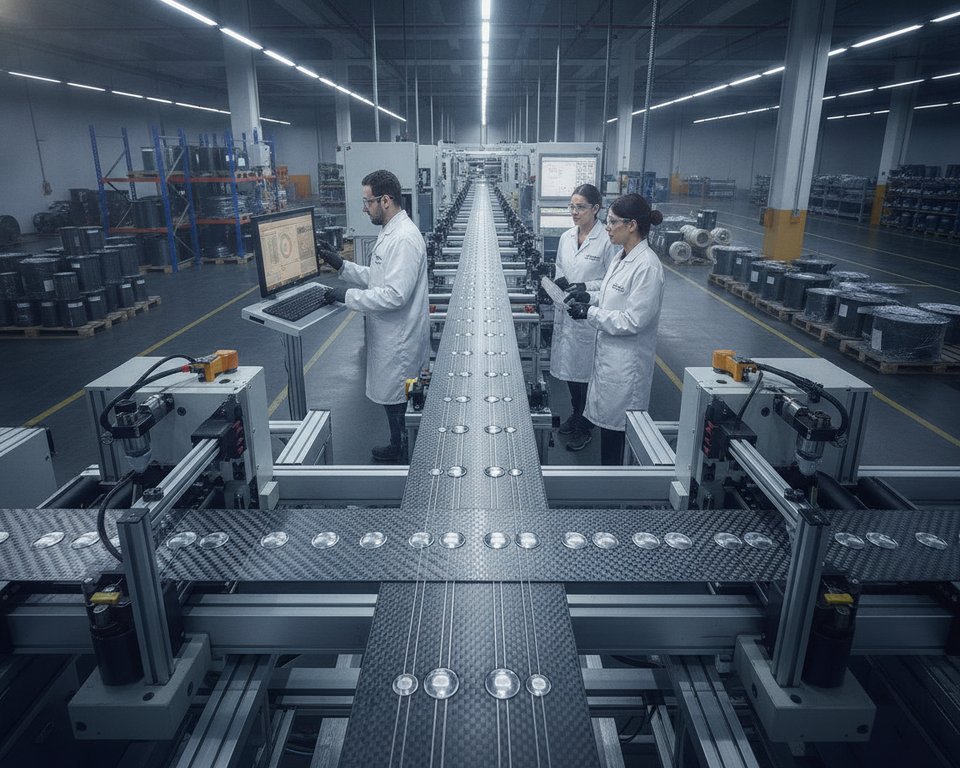 Intermittent Bonded Ribbon Production Line
| Ribbon Design Feature | Flexible Bonded Design | Traditional Continuous Ribbon |
|---|---|---|
| Bond pattern | Separated bonds at controlled intervals | Bonding maintained continuously along the ribbon |
| Fiber configuration between bond points | Can bend, roll, or fold for dense packing | Maintains a largely fixed flat profile |
| Splicing configuration | Can return to a flat format for mass fusion splicing | Already held in a fixed flat ribbon form |
| Cable packing role | Allows compact and flexible subunit positioning | Typically uses a fixed ribbon stack configuration |
| Common cable use | Flexible flat cable and high-density fiber cable designs | Standard flat ribbon cable designs |
Construction And Material Requirements For Intermittent Bonded Ribbon
An intermittent bonded ribbon integrates precise fiber placement with adaptable bonding points. Its architecture facilitates dense cable configurations while allowing effortless separation during handling, routing, and splicing.
Choosing appropriate materials significantly influences ribbon width, peel characteristics, and durability. Each optical fiber subunit must maintain its fibers securely without imparting undue stiffness to the ribbon.
Optical Fiber Counts And Subunit Layout
Flexible bonded ribbons may support 4, 8, 12, 24, or up to 36 fibers. The choice of fiber count is determined by cable capacity, available duct space, and the requirements of subsequent mass fusion splicing.
A 12-fiber configuration often employs six subunits, with two adjacent fibers in each subunit. The fibers within a subunit may be in contact or separated by no more than one and a half times the fiber diameter.
Small gaps placed between subunits ensures ribbon flexibility. These gaps typically span from 5 to 100 micrometers, while the fibers remain aligned side by side across the ribbon width.
| Construction Feature | Typical Arrangement | Manufacturing Purpose |
|---|---|---|
| Fiber count | 4, 8, 12, 24, or as many as 36 fibers | Supports required cable density and fusion splice capacity |
| Subunit configuration | Two adjacent fibers per optical fiber subunit | Allows controlled separation between fiber groups |
| Subunit fiber spacing | Fibers touching or separated by up to 1.5 diameters | Supports a small and consistent subunit profile |
| Gap between subunits | 5 to 100 micrometers | Allows greater movement and flexibility near bond points |
UV-Curable Resin And Wet-On-Wet Bonding
The coating and bond systems frequently employ UV-curable resin systems. Wet-on-wet bonding involves applying the bond material to the uncured subunit coating, which then cures together under UV energy.
Wet-on-wet bonding produces a diffusion zone where the materials interact. For intermittent bonded ribbons, this zone can range from 2 to 50 micrometers, with 5 to 15 micrometers being the typical focused process range.
UV-curable resin materials can blend at the interface before curing. This encourages molecular entanglement between the bond and the optical fiber subunit coating, resulting in bonds that are both secure and flexible.
Main Equipment For Intermittent Bonded Ribbon Production
An optical ribbon line integrates advanced motion control with meticulous material handling. Each station ensures fibers remain aligned, clean, and stable from the initial payoff to the final winding.
The line equipment manages adjacent fiber placement, subunit coating, intermittent bonding, UV curing, cooling, inspection, and take-up. This sequential process enables manufacturers to produce flexible custom ribbon cable, preserving the integrity of the fiber order.
Fiber Payoff With Tension Control
Fiber payoff systems feed individual optical fibers at a consistent rate from spools. Guides, rollers, and tension sensors prevent sudden pulls, averting twist, slack, or uneven spacing.
During ribbon production, maintaining balanced fiber paths before alignment is critical. Stable tension is essential for forming flat subunits and ensuring accurate color sequence control.
Discrete Bond Applicator And Coating Die
A coating die places a UV-curable material around groups of two or more fibers. This material defines subunits while maintaining fibers in a flat, parallel layout.
The discrete bond applicator subsequently deposits a second resin between neighboring subunits at planned intervals. This spacing allows the ribbon to flex and separate when needed, a critical aspect of custom ribbon cable design.
| Production Equipment | Primary Function | Process Benefit |
|---|---|---|
| Payoff tension system | Delivers fibers while maintaining regulated tension | Minimizes twisting and uneven fiber loading |
| Coating die | Creates coated optical fiber subunits | Supports stable subunit width and geometry |
| Intermittent bond applicator | Deposits resin at set intervals | Provides controlled flexible bonds between subunits |
| UV curing, cooling, and take-up unit | Cures and cools the ribbon before inspection and winding | Protects bond quality and preserves fiber order |
UV Curing, Cooling, And Ribbon Take-Up Equipment
UV energy cures the subunit coating and intermittent bonds while the resin is wet. This wet-on-wet process forms a cohesive interface between materials, influencing bond strength.
Cooling equipment lowers ribbon temperature before inspection and winding. The fiber ribbon line may also employ vision checks to monitor width, bond position, and surface quality.
Take-up equipment winds the finished ribbon with low, even tension. Proper winding preserves the finished bonded structure, ensuring the custom ribbon cable is ready for later cabling, splicing, or connector assembly.
Fiber Preparation, Alignment, And Color Sequence Control
Reliable ribbon cable production starts with fiber preparation. Each strand must enter the assembly clean, centered, and in the correct sequence before the coating and bonding processes commence.
Managing Fiber Identification During Splicing And Maintenance
Consistent fiber color identification is indispensable for splicing, testing, and maintenance operations. The standard 12-fiber sequence, typically consisting of blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua, facilitates swift identification.
When fiber counts increase, the sequence may be repeated within controlled subunits. This method ensures that each ribbon cable remains organized within splice trays, closures, and cable connector layouts.
| Fiber Number | Fiber Identification Color | Process Purpose |
|---|---|---|
| 1 | Standard blue | Marks the first position in the standard color order |
| 2 | Standard orange | Provides rapid visual identification |
| 3 | Standard green | Helps preserve the established fiber order |
| 04 | Brown | Helps verify subunit placement |
| 05 | Standard slate | Provides distinct mid-sequence marking |
| 6 | White | Improves visibility during inspection |
| 07 | Standard red | Improves traceability in splicing records |
| 8 | Black | Helps technicians recognize sequence position in trays |
| 09 | Standard yellow | Aids field restoration work |
| Position 10 | Standard violet | Helps distinguish later positions in the standard sequence |
| 11 | Standard rose | Helps maintain clarity in higher-count ribbon layouts |
| 12 | Aqua | Finishes the standard 12-fiber color sequence |
Preventing Fiber Twisting And Uneven Tension
Payoff units and guides are instrumental in maintaining fibers in a flat, side-by-side configuration. This prevents twist, crossing, and gaps that could alter the ribbon’s width or distort the bond pattern.
Production personnel carefully check tension across every path before the fibers reach the coating die. Proper alignment is critical for mass fusion splicing and ensures the finished ribbon cable fits its intended cable connector system.
Intermittent Bond Application And UV Curing Process
Intermittent bonding connects fiber subunits without solidifying the ribbon into a rigid form. This method facilitates compact routing and ensures dependable handling within a flexible flat cable. It also aids in maintaining the planned fiber layout during subsequent cable assembly.
Applying Bonds At Predetermined Intervals
Bond applicators place resin at intervals ranging from 10 mm to 1,000 mm. The bond locations may stagger along the ribbon’s length. This arrangement provides support to adjacent subunits while allowing sufficient free length for movement.
The bond applicator delivers a measured amount of UV-curable resin at each bond point. Bonds often exhibit a diamond-like shape, with wider centers and narrower ends. The tapered ends reduce sudden stress transitions when the cable bends or twists.
Creating Flexible And Strong Bond Interfaces
Wet-on-wet bonding involves applying a second material before the first subunit coating cures. The uncured layers can blend before undergoing a shared UV curing step. This approach fosters a gradual interface, unlike a sharp material boundary.
The resulting material gradient affects various properties, including color, Young’s modulus, and surface friction. Bond ends may feature saddle-like surfaces with both convex and concave curves. These features improve resistance to bond peeling while facilitating separation when required.
Controlling Curing Performance
The UV lamps must supply consistent energy across the ribbon. Factors such as line speed, lamp output, resin volume, and exposure time impact the bond’s quality. Selecting the right UV-curable resin ensures rapid curing without compromising the fiber coating.
Process personnel carefully track bond shape, cure level, and ribbon flexibility during production. The cured cable should transition smoothly from a flat plane to various forms without bond damage. Controlled curing ensures consistent handling throughout winding and downstream processing.
Quality Control For Flexible Flat Cable And Fiber Ribbon Output
Maintaining the integrity of each flat ribbon cable is a meticulous process. It involves checking the cable’s flexibility and its readiness for subsequent splicing operations. During production, operators assess the fiber count, color sequence, and precise positioning of each fiber. They also evaluate the cable’s winding condition, ensuring its optimal state for assembly.
Routine inspection is essential in identifying any defects in the coating, uneven tension, or misplaced bonds. These issues, if left unaddressed, could compromise the cable’s performance in subsequent stages of production.
Inspection Of Bond Spacing, Ribbon Width, And Thickness
The spacing between bonds is a critical parameter, requiring adherence to a specific design range. This spacing is essential for the cable’s flexibility, ensuring that the fibers remain aligned within their designated subunits during bending.
Inspection protocols are in place to confirm that each bond correctly connects adjacent subunits. This attention to detail ensures that the ribbon lays flat, facilitating smooth mass fusion splicing processes.
| Inspection Point | Items Checked | Production Value |
|---|---|---|
| Fiber sequence identification | Fiber number, color order, and placement | Helps ensure accurate splicing and maintenance |
| Bond pattern | Bond position, interval, and connection between subunits | Supports organized fibers without sacrificing flexibility |
| Ribbon profile | Width, thickness, and flatness | Supports compatibility with handling and splice equipment |
| Surface condition | UV curing condition, coating coverage, and surface defects | Reduces handling damage during winding |
Optical And Mechanical Performance Testing
Mechanical testing focuses on bond separation, cohesive strength, elongation, and handling behavior. These evaluations are essential to confirm that the manufacturing process controls are consistent across similar designs of flat cables.
Optical testing encompasses evaluations after bonding and curing. It ensures that the core, cladding, primary coating, secondary coating, and color layer are adequately protected throughout the manufacturing process.
Attenuation measurements and splice-handling tests are integral to routine inspections. The quality of winding is also scrutinized to ensure that the finished flat ribbon cable is in a controlled condition for assembly.
Precision Winding, Automation, And Production Efficiency
High-efficiency ribbon production relies on a unified production line. Each stage, from fiber payoff to inspection and take-up, must harmonize seamlessly. This synchronization ensures the preservation of fiber geometry and facilitates consistent output, critical for high-speed data transmission cables.
Line Synchronization And Process Data Monitoring
Control systems integrate payoff speed, fiber tension, resin delivery, bond placement, UV curing, cooling, and take-up. Adjustments are made in real time to maintain ribbon stability when speed variations occur at any station.
Production records track fiber color sequences, bond intervals, cure settings, ribbon dimensions, and winding status. This detailed history allows operators to track the production of each custom ribbon cable.
- Payoff tension prevents fiber stretch and slack.
- Controlled bond timing maintains regular intervals between bond points.
- Dimensional checks detect width or thickness deviations promptly.
- Winding records support lot traceability and downstream handling.
Winding Ribbon For Downstream Cable Production
A precision cable winder helps ensure the ribbon is wound onto a spool with uniform tension and controlled movement. This method prevents edge crushing, layer crossing, and sudden pulls during subsequent cable processing.
Finished ribbon structures may be stacked, rolled, or loaded into central tube and loose tube designs. These configurations enable the creation of high-speed data transmission cables, even in areas where duct additions are impractical.
When producing custom ribbon cable, the winding pattern must align with subsequent processes. Proper spool buildup is essential for smooth payout during stranding, tube loading, and cable assembly.
| Monitoring Area | Primary Control Focus | Resulting Benefit |
|---|---|---|
| Optical fiber payoff | Stable tension and correct color sequence | Consistent ribbon organization during cable assembly |
| Bond application | Consistent spacing and resin volume | Consistent flexible behavior in downstream operations |
| UV cure stage | Regulated UV intensity and exposure duration | Properly cured bonds before ribbon winding |
| Cable winding system | Uniform traverse with controlled spool tension and layering | Smooth payout for central tube or loose tube loading |
Ribbon Cable Applications, Fusion Splicing, And Connector Planning
Ribbon fiber is widely used in dense links within data centers, telecom backbones, metro rings, and FTTx feeder routes. It also excels in indoor FTTH runs, 5G fronthaul, and outdoor point-to-point networks where space is at a premium.
A meticulously planned ribbon cable assembly enables crews to manage high fiber counts efficiently, without increasing bulk. Each high-speed data transmission cable must align with the site’s route, enclosure space, and future expansion plans.
Mass Fusion Splicing Advantages
A ribbon fusion splicer allows the joining of an entire ribbon in a single operation. For a 12-fiber ribbon, a matching cleaver can prepare all 12 fibers simultaneously before the automated fusion process commences.
Mass fusion processing lowers handling time and ensures consistent fiber alignment. Splice loss is reported to remain below 0.05 to 0.10 dB per fiber, contingent upon controlled preparation, cleaning, and machine settings.
Loose tube cable, on the other hand necessitates a different strategy at the splice cassette. Technicians must separate the fibers, then splice them individually, which prolongs the ribbon cable assembly process.
Dense Link Connection Planning
High-density fiber links often employ MPO or MTP trunks, harnesses, fanout cables, and cassette modules. The chosen cable connector must align with the fiber count, polarity method, connector gender, and fiber type.
System planning must also account for transceiver requirements and the full link loss budget. A high-speed data transmission cable, when used with parallel optics, demands a clear polarity path from equipment port to patch panel.
| Planning Item | Primary Control | Common Application |
|---|---|---|
| Number of ribbon fibers | Required splice capacity and cassette configuration | Backbone links using 12-fiber or 24-fiber ribbons |
| MPO/MTP cable connector | Connector polarity, gender, and port compatibility | Data center trunk links and 5G equipment areas |
| Harness or fanout cable | Transition from multi-fiber connections to single-fiber ports | Network switch connections and patch fields |
| Link loss budget | Permitted optical loss across splices, connectors, and fiber | High-speed data transmission cable routes |
Shanghai Weiye OFC Equipment For Fiber Ribbon Production Lines
Shanghai Weiye OFC Equipment, also known as SHWY, specializes in machinery for the production of optical fibers and cables, serving markets in the United States and globally. Its offerings are designed to maintain stable production, facilitate clear operator control, and enable seamless integration into production lines.
For initiatives requiring an intermittent bonded ribbon production line, SHWY equips each phase of ribbon handling, curing, and winding with suitable machinery.
SHWY Optical Fiber And Cable Machinery Experience
Established in 1998, SHWY’s journey in the industry has been marked by significant milestones. By 2012, its annual turnover surpassed 200 million CNY, strengthening its position within a prominent Chinese fiber and cable conglomerate as a joint venture.
In 2020, SHWY transitioned to independence, relocating to a state-of-the-art facility in central Shanghai. This move underscored its commitment to advancing equipment research, manufacturing, and process application while supporting operational stability.
SHWY Production Equipment Portfolio
SHWY offers a diverse range of equipment, including fiber draw towers, coloring machines, secondary coating lines, SZ stranding equipment, and cable sheathing lines. Notably, it also features a fiber ribbon line tailored for flat, high-count fiber formats.
Within ribbon cable production, a cable precision winder plays a critical role in maintaining orderly package buildup and controlled tension. This ensures safer transport and more consistent feeding into subsequent cable production stages.
Additional SHWY equipment includes FTTH lines, indoor cable equipment, and OPGW fiber-in-stainless-steel-tube systems. These options enable manufacturers to integrate an intermittent bonded ribbon production line with complementary cable processes.
Final Thoughts
A complete intermittent bonded ribbon line brings together fiber alignment, controlled bonding, UV curing, inspection, and precision winding into a unified process. Each step maintains organized fiber positioning while maintaining the necessary bendability for dense cable designs. This combination is critical for the creation of high-density optical networks.
The resultant ribbon cable supports efficient mass fusion splicing and organized fiber management. It is ideal for applications with high fiber counts, confined ducts, limited tray space, and frequent splice points. This makes it a cornerstone in many high-density ribbon cable routes.
Comprehensive project planning reaches beyond the production line. It encompasses the cable structure, closure capacity, fusion tools, test methodologies, labeling, and restoration records. These elements must align with the planned network architecture for seamless integration.